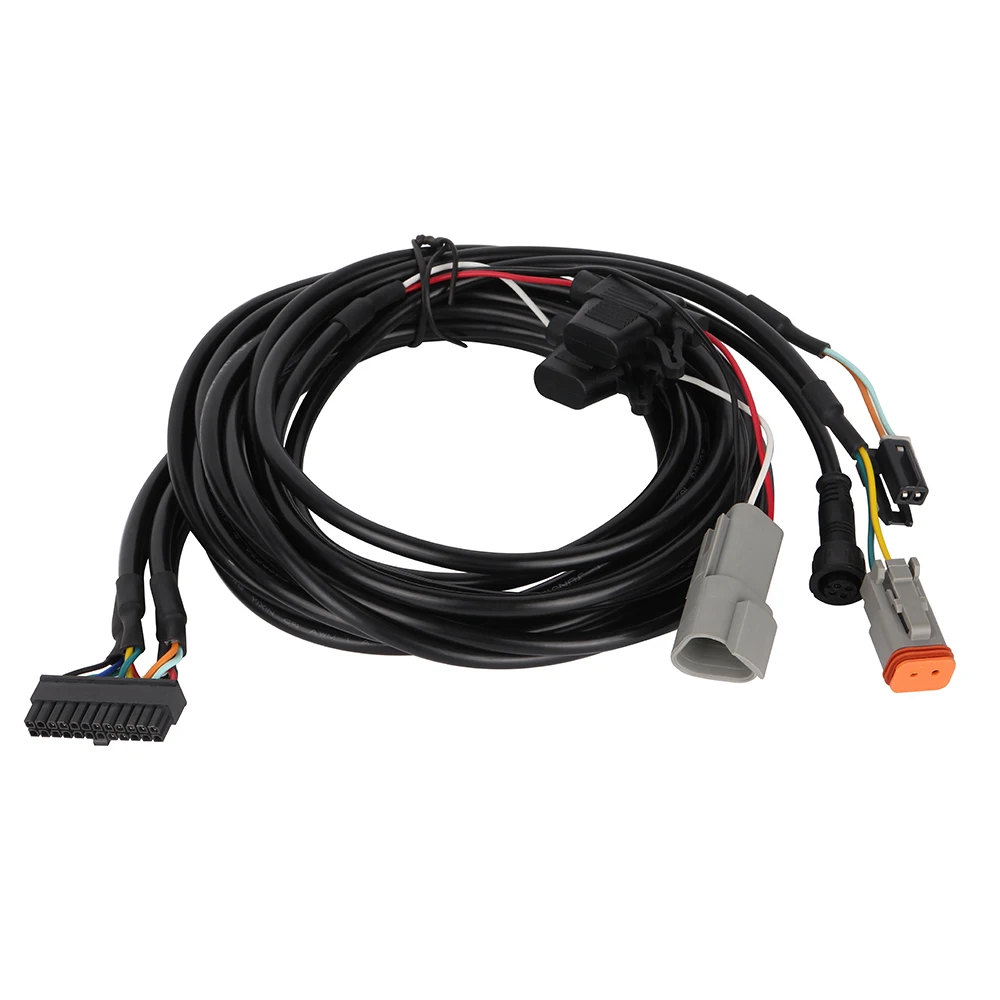
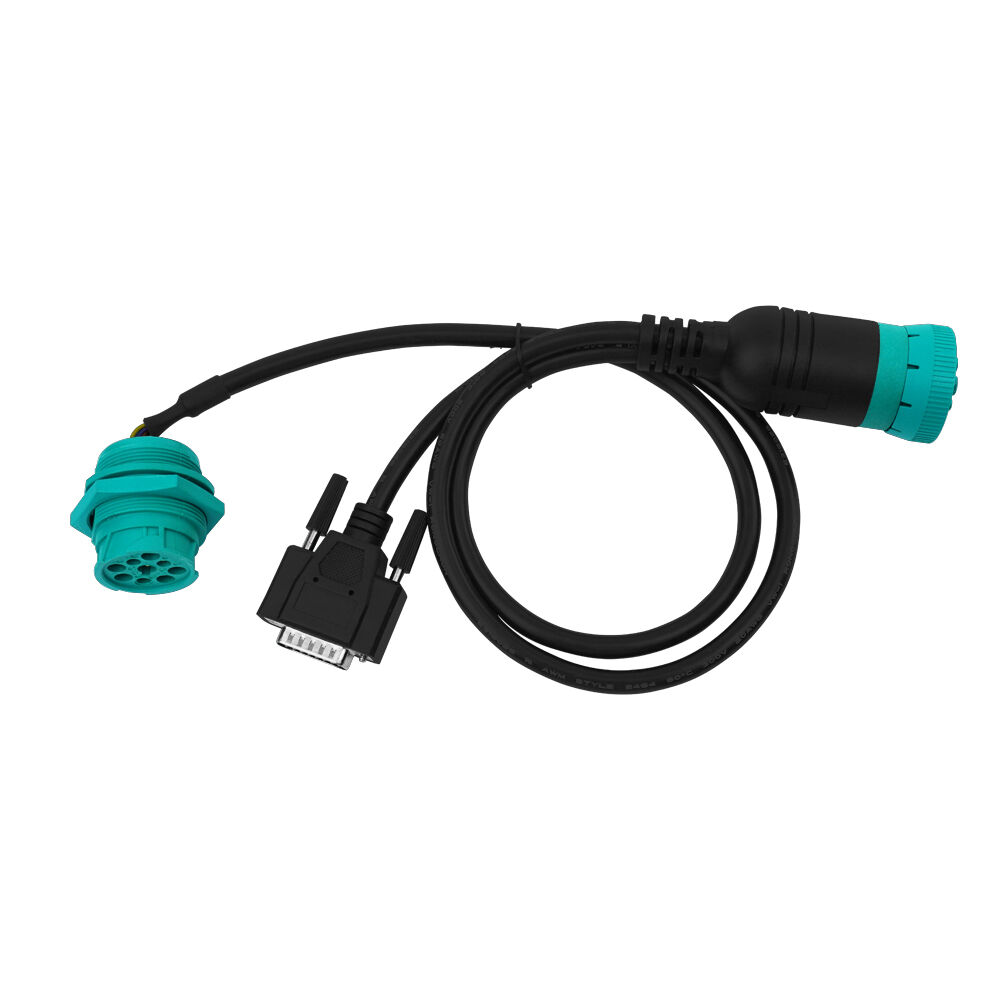
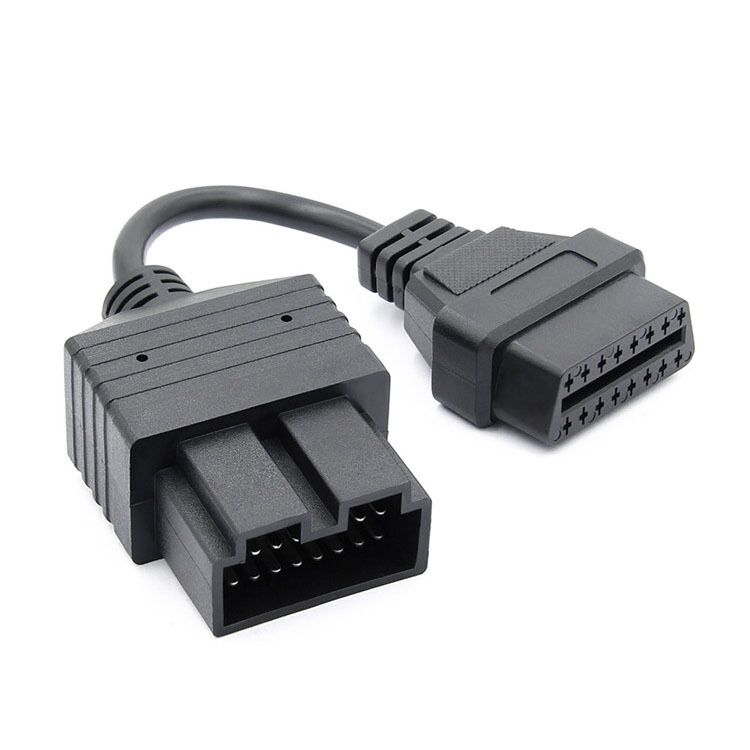
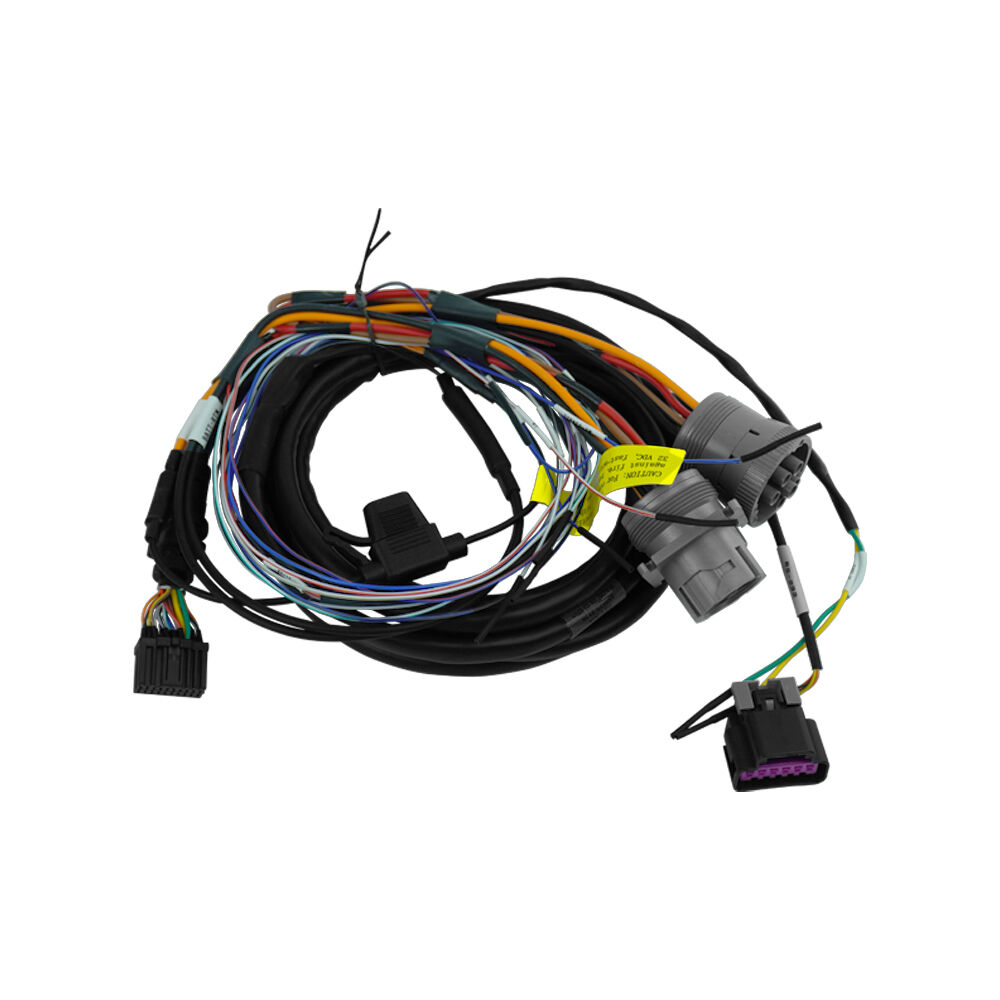
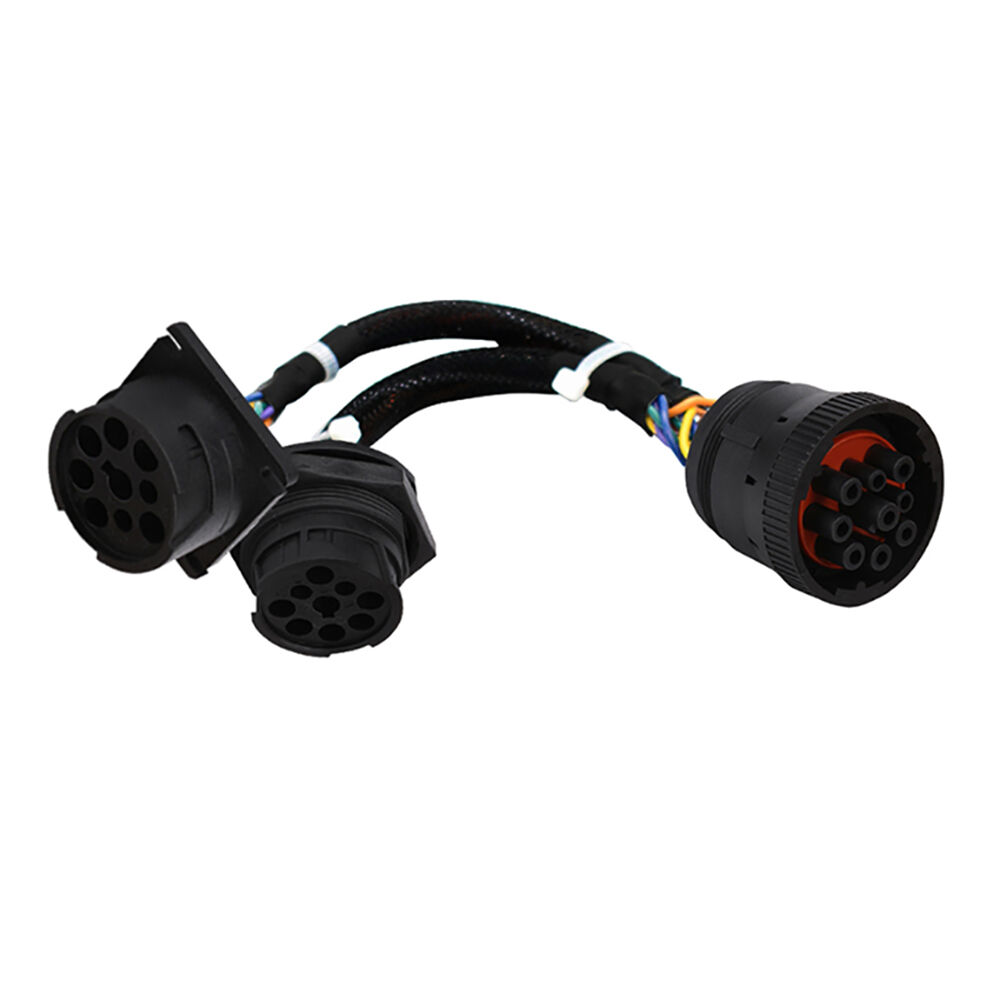
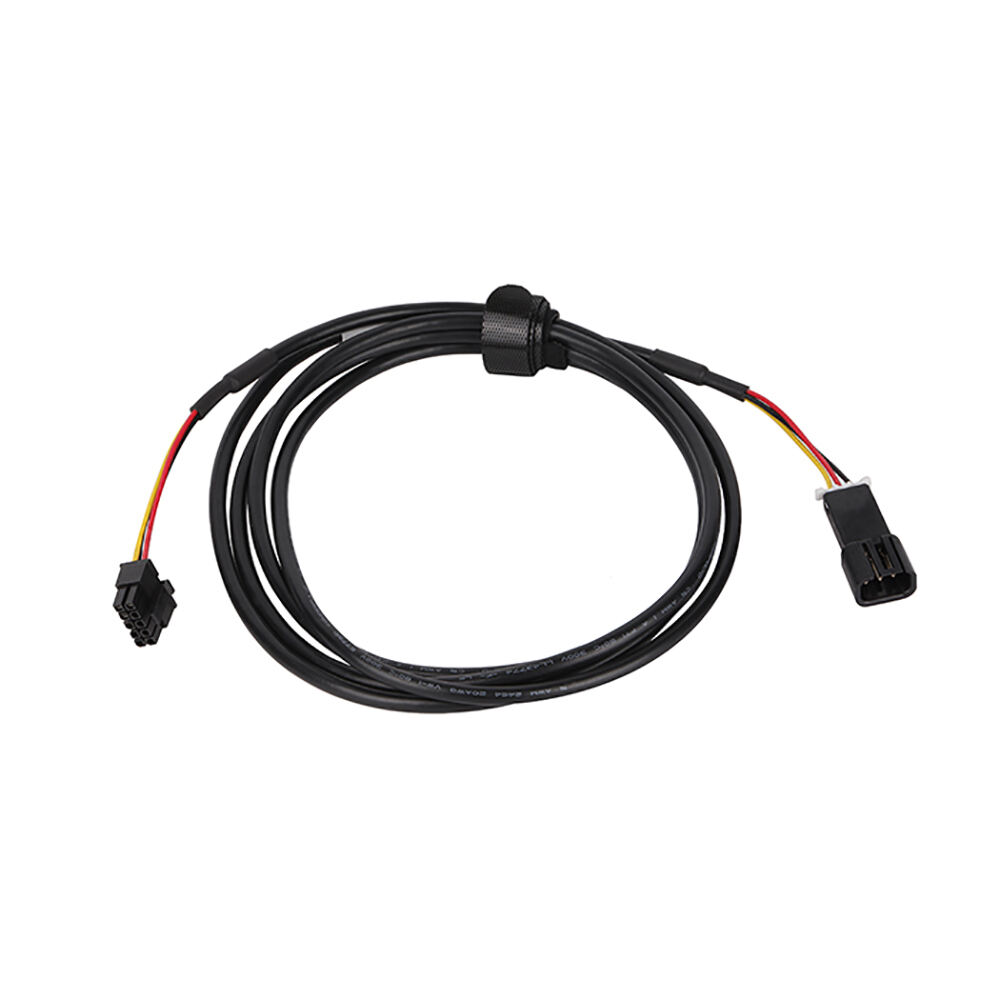
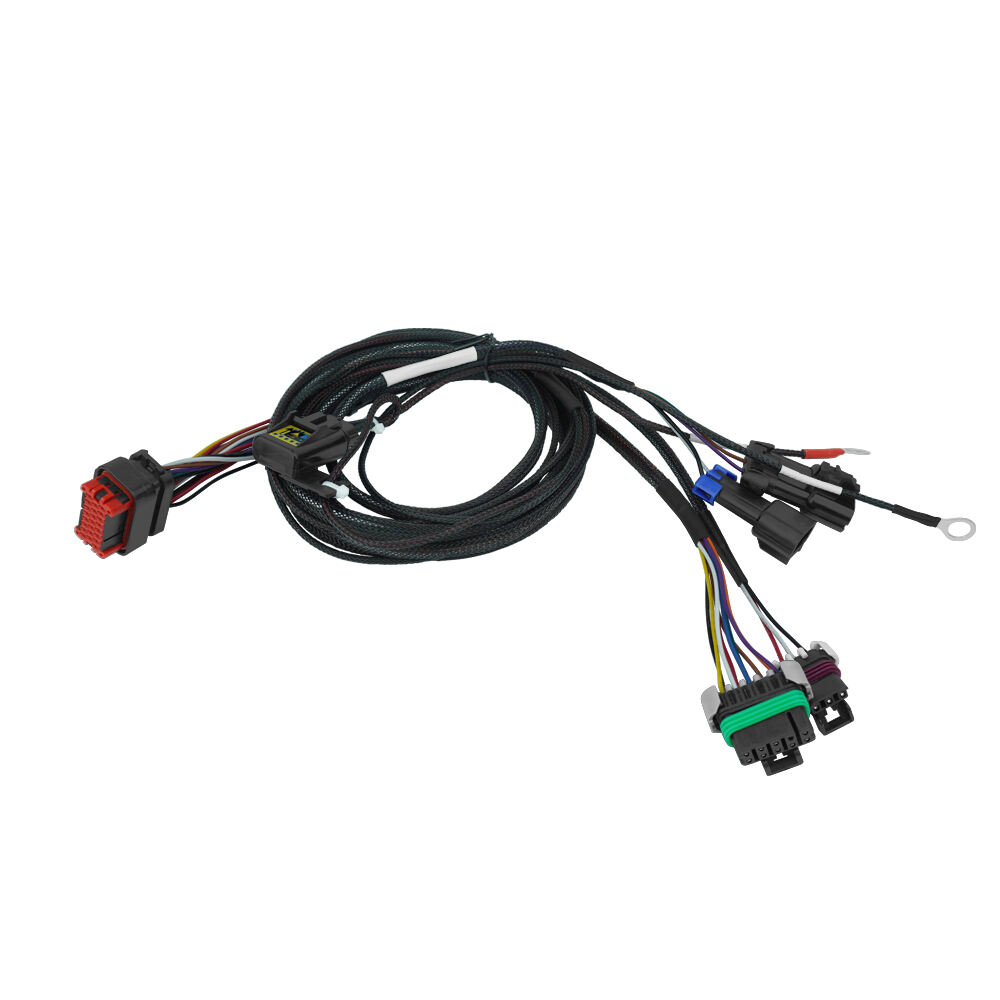
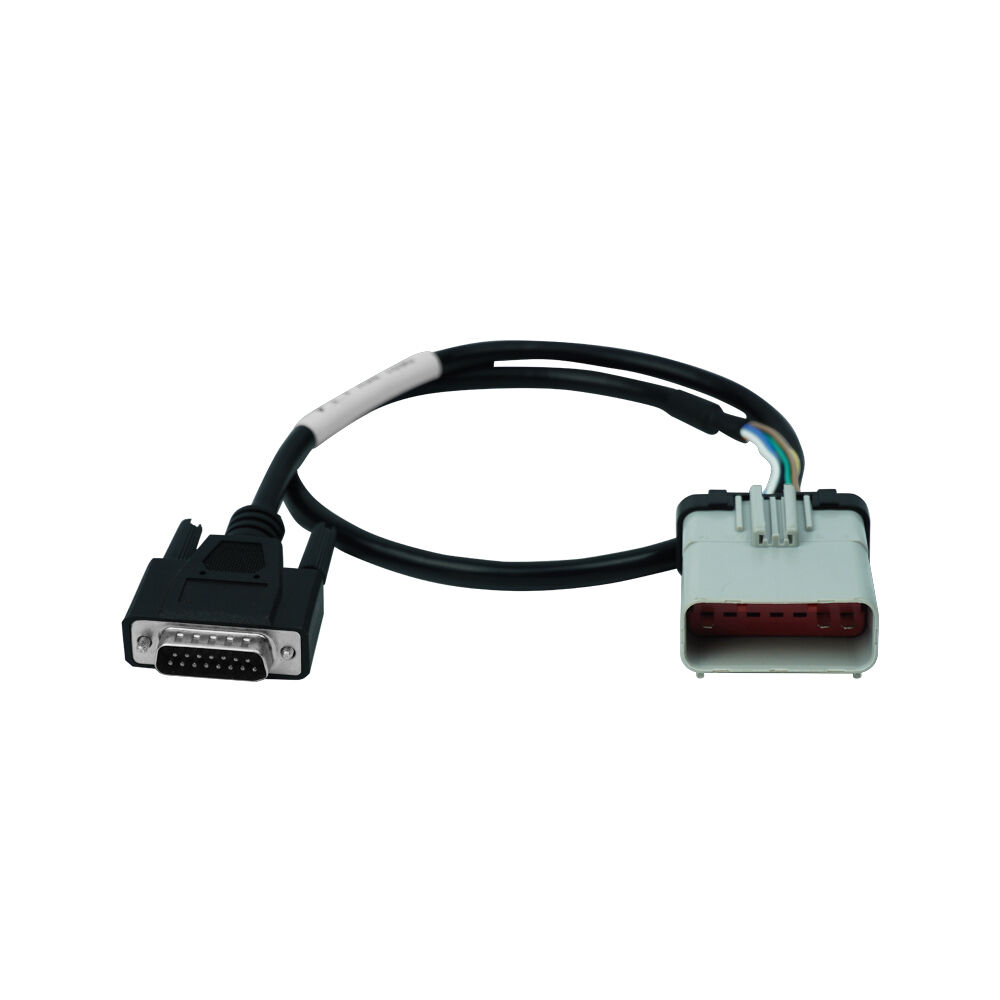
Premium Waterproof Cable Sleeve Solutions - Complete Protection for Electrical Connections

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

waterproof cable sleeve

A waterproof cable sleeve represents an essential protective solution designed to safeguard electrical cables and wire connections from moisture, water ingress, and environmental hazards. This specialized protective component serves as a critical barrier that prevents water damage, corrosion, and electrical failures in various installation environments. The waterproof cable sleeve functions by encapsulating cable joints, splices, and termination points within a sealed enclosure that blocks moisture penetration while maintaining electrical integrity. Manufactured from durable materials such as heat-shrinkable polymers, rubberized compounds, or reinforced plastics, these sleeves provide reliable protection across diverse operating conditions. The technological foundation of a waterproof cable sleeve incorporates multiple protective layers that work synergistically to deliver comprehensive defense against water exposure. Advanced sealing mechanisms including adhesive linings, compression fittings, and thermal activation processes ensure complete encapsulation of vulnerable cable areas. Modern waterproof cable sleeve designs feature enhanced flexibility that accommodates cable movement without compromising seal integrity, while maintaining resistance to temperature fluctuations, chemical exposure, and physical abrasion. Applications for waterproof cable sleeve solutions span numerous industries and environments where moisture protection proves essential. Outdoor electrical installations, underground cable networks, marine equipment, automotive wiring systems, irrigation controls, landscape lighting, industrial machinery, telecommunications infrastructure, and renewable energy systems all benefit from waterproof cable sleeve implementation. The versatility of these protective components allows customization for specific cable dimensions, voltage requirements, and environmental conditions. Installation procedures for waterproof cable sleeve products emphasize simplicity and reliability, enabling both professional electricians and skilled operators to achieve secure moisture barriers efficiently. The protective performance of a waterproof cable sleeve directly impacts system longevity, operational safety, and maintenance costs, making it an indispensable component for any electrical installation exposed to wet or humid conditions.

New Product Releases

Choosing a waterproof cable sleeve delivers substantial practical benefits that protect your investment and ensure reliable electrical performance over extended service periods. The primary advantage centers on preventing water damage that causes expensive equipment failures, system downtime, and safety hazards. When moisture infiltrates cable connections, oxidation and corrosion rapidly degrade conductivity, leading to overheating, short circuits, and complete connection failure. A waterproof cable sleeve eliminates these risks by creating an impenetrable barrier that keeps connections dry and functional regardless of weather conditions or environmental exposure. This protection translates directly into reduced maintenance requirements and lower total ownership costs, as protected connections remain stable and require minimal intervention over their operational lifespan. The financial savings from avoiding premature cable replacement, emergency repairs, and equipment damage quickly offset the modest initial investment in quality waterproof cable sleeve products. Beyond moisture protection, these sleeves provide mechanical reinforcement that strengthens vulnerable connection points against physical stress, vibration, and accidental impact. This dual protective function proves especially valuable in demanding applications where cables experience movement or environmental stress. Installation simplicity represents another significant advantage, as most waterproof cable sleeve designs require no specialized tools or extensive technical training. Users can achieve professional-grade protection through straightforward application procedures that minimize installation time and labor costs. The flexibility inherent in quality waterproof cable sleeve construction accommodates various cable sizes and configurations, providing versatile solutions for diverse project requirements without necessitating extensive inventory management. Temperature resilience ensures consistent protection across seasonal variations and extreme operating conditions, maintaining seal integrity whether facing freezing winters or scorching summers. The chemical resistance built into premium waterproof cable sleeve materials defends against corrosive substances, oils, and solvents commonly encountered in industrial and outdoor environments. This comprehensive protection extends cable service life significantly, often doubling or tripling the operational duration compared to unprotected installations. Safety improvements constitute a critical advantage, as properly protected electrical connections reduce fire risks, electrocution hazards, and system failures that might endanger personnel or property. Regulatory compliance becomes simpler when using waterproof cable sleeve solutions that meet industry standards for moisture protection and electrical safety. The visual confirmation provided by installed sleeves allows easy inspection and verification of protected connections during routine maintenance checks. Environmental sustainability benefits emerge from extended equipment lifespan and reduced material waste associated with premature cable replacement. These combined advantages make waterproof cable sleeve adoption a practical decision that enhances system reliability while controlling operational expenses.

Practical Tips

What are the key application scenarios and advantages of J1939 connection cables in industrial automation?

10

Feb

What are the key application scenarios and advantages of J1939 connection cables in industrial automation?

Industrial automation has revolutionized manufacturing and heavy machinery operations, with standardized communication protocols playing a crucial role in ensuring seamless data exchange between electronic control units. Among these protocols, J1939 ...
View More
How does J1939 connection cable ensure efficient and stable data transmission in commercial vehicles?

10

Feb

How does J1939 connection cable ensure efficient and stable data transmission in commercial vehicles?

Commercial vehicles rely heavily on sophisticated diagnostic and communication systems to ensure optimal performance, safety, and regulatory compliance. At the heart of these systems lies the J1939 connection cable, a specialized diagnostic interface...
View More
What Connector Types Are Compatible with Standard J1939 Connection Cable Applications?

02

Apr

What Connector Types Are Compatible with Standard J1939 Connection Cable Applications?

Standard J1939 connection cable applications require specific connector types that ensure reliable communication between electronic control units in heavy-duty vehicles and industrial equipment. Understanding which connector configurations work with ...
View More
What advantages do OEM-grade Tesla wiring harnesses provide over generic alternatives?

17

Apr

What advantages do OEM-grade Tesla wiring harnesses provide over generic alternatives?

When considering electrical components for Tesla vehicles, the choice between OEM-grade Tesla wiring harnesses and generic alternatives represents a critical decision that impacts performance, reliability, and long-term vehicle integrity. Tesla wirin...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

waterproof cable sleeve

Superior Moisture Barrier Technology

Superior Moisture Barrier Technology

The moisture barrier technology integrated into advanced waterproof cable sleeve designs represents a sophisticated engineering achievement that delivers uncompromising protection against water intrusion. This protective capability stems from multi-layer construction that combines specialized materials with precision sealing mechanisms to create an impenetrable defense around vulnerable cable connections. The outer layer typically consists of robust polymeric materials that resist punctures, abrasions, and environmental degradation while providing the initial barrier against water contact. Beneath this protective shell, adhesive sealant layers activate through heat application or mechanical compression, flowing into microscopic gaps and irregularities to eliminate potential moisture pathways. This adhesive technology creates molecular-level bonding with cable insulation and conductor surfaces, establishing a continuous seal that remains intact despite thermal cycling, vibration, and flexing. The waterproof cable sleeve moisture barrier maintains effectiveness across extreme temperature ranges, preventing seasonal expansion and contraction from compromising seal integrity. Advanced formulations incorporate hydrophobic compounds that actively repel water molecules, ensuring that even prolonged submersion or pressure washing cannot force moisture past the protective barrier. This technology proves essential for underground cable installations where groundwater saturation creates constant moisture pressure against protective components. Marine applications benefit tremendously from this moisture barrier technology, as saltwater exposure accelerates corrosion processes that rapidly destroy inadequately protected connections. The waterproof cable sleeve barrier prevents electrolytic reactions between dissimilar metals in cable assemblies, eliminating galvanic corrosion that undermines connection integrity. Testing protocols for premium waterproof cable sleeve products include submersion trials, pressure testing, and accelerated aging simulations that verify long-term barrier performance under demanding conditions. The practical implications of superior moisture barrier technology extend beyond simple water exclusion to encompass preservation of electrical characteristics including resistance values, insulation properties, and current-carrying capacity. When connections remain dry and corrosion-free, electrical systems operate at design specifications throughout their intended service life, avoiding performance degradation that compromises efficiency and reliability. Installation quality significantly influences moisture barrier effectiveness, making proper application techniques essential for achieving specified protection levels. Comprehensive waterproof cable sleeve designs incorporate visual indicators and tactile feedback mechanisms that confirm correct installation and complete seal activation. The investment in superior moisture barrier technology pays dividends through decades of trouble-free operation, eliminating the recurring costs and operational disruptions associated with moisture-related cable failures in demanding environments.
Versatile Application Compatibility

Versatile Application Compatibility

The versatile application compatibility of modern waterproof cable sleeve solutions addresses the diverse protection requirements encountered across residential, commercial, industrial, and specialized installation environments. This adaptability stems from thoughtful engineering that accommodates varying cable dimensions, conductor configurations, voltage levels, and environmental exposure conditions within a cohesive product family. A quality waterproof cable sleeve system offers multiple size options that fit cable diameters ranging from small control wiring to substantial power distribution conductors, ensuring appropriate solutions exist for virtually any electrical connection requiring moisture protection. The material formulations used in these sleeves balance flexibility and structural integrity, allowing conformance to irregular connection geometries while maintaining protective capabilities. This versatility proves invaluable when protecting cable splices, terminations, branch connections, and repair sections that present unique dimensional challenges. Temperature tolerance represents a critical aspect of application compatibility, as waterproof cable sleeve products must function reliably whether installed in refrigerated facilities, desert environments, or equipment enclosures experiencing significant heat generation. Premium sleeve materials maintain sealing properties and mechanical strength across temperature ranges spanning negative forty to positive eighty degrees Celsius, ensuring consistent protection regardless of climatic conditions. The chemical compatibility of advanced waterproof cable sleeve compounds extends application possibilities into industrial settings where exposure to petroleum products, cleaning solvents, fertilizers, and processing chemicals might compromise inferior protective materials. Agricultural irrigation systems, chemical processing facilities, petroleum refineries, and manufacturing plants all present challenging chemical environments that demand robust protective solutions. A waterproof cable sleeve designed for broad application compatibility incorporates UV stabilizers that prevent degradation from prolonged sunlight exposure, essential for outdoor installations and above-ground cable runs. The mechanical flexibility inherent in versatile waterproof cable sleeve designs accommodates cable movement resulting from thermal expansion, settling, vibration, or intentional relocation without seal failure or material fracture. This flexibility proves particularly valuable in mobile equipment applications, robotic systems, and installations subject to building movement or ground shifting. Electrical compatibility considerations ensure waterproof cable sleeve materials provide adequate dielectric strength and insulation resistance for the voltage levels present in protected circuits, from low-voltage control wiring to medium-voltage distribution systems. The installation methodology for versatile waterproof cable sleeve products adapts to field conditions, offering options for heat-shrink application, cold-applied wrapping, or mechanical compression depending on available tools and environmental constraints. This installation flexibility allows effective cable protection in remote locations, confined spaces, energized environments, and weather-limited outdoor settings where conventional protection methods prove impractical. Regulatory compliance across multiple industry standards and international specifications demonstrates the broad application compatibility of professionally engineered waterproof cable sleeve solutions, simplifying specification and procurement for projects spanning diverse jurisdictions and industry sectors.
Extended Service Life Performance

Extended Service Life Performance

The extended service life performance delivered by premium waterproof cable sleeve implementations represents a compelling value proposition that transforms initial product costs into long-term economic advantages through decades of reliable protection. This longevity stems from careful material selection, robust construction techniques, and comprehensive protection against the degradation mechanisms that limit the operational lifespan of electrical connections. When properly installed, a quality waterproof cable sleeve can protect cable connections for twenty to thirty years or more, often matching or exceeding the service life of the cables themselves. This durability eliminates the recurring expenses associated with connection refurbishment, reducing lifecycle costs and minimizing operational disruptions from maintenance activities. The foundation of extended service life performance lies in resistance to environmental stressors including UV radiation, thermal cycling, moisture exposure, chemical contact, and mechanical wear. Premium waterproof cable sleeve materials incorporate stabilizers and reinforcements that prevent polymer degradation, maintaining mechanical properties and sealing effectiveness throughout extended outdoor exposure. The molecular structure of advanced sleeve compounds resists oxidation processes that cause embrittlement and cracking in inferior materials, ensuring the protective barrier remains intact and flexible over decades of service. Thermal stability proves essential for extended performance, as repeated heating and cooling cycles stress protective components through expansion and contraction. A properly engineered waterproof cable sleeve accommodates these thermal movements without developing gaps or separation at critical sealing interfaces, maintaining moisture protection regardless of temperature fluctuations. The adhesive systems used in premium waterproof cable sleeve products maintain bonding strength throughout the service life, resisting creep, degradation, and adhesion loss that might compromise seal integrity over time. This adhesive longevity stems from formulations specifically developed for electrical applications where long-term reliability outweighs considerations of easy removal or repositioning. Mechanical robustness contributes significantly to extended service life, as waterproof cable sleeve installations often experience accidental impacts, abrasion from adjacent components, and stress from cable movement. Reinforced construction and impact-resistant materials protect the moisture barrier from physical damage that might otherwise create penetration points for water intrusion. The corrosion prevention provided by effective waterproof cable sleeve protection directly extends cable service life by eliminating the electrochemical reactions that destroy conductor surfaces and compromise connection integrity. This protection proves especially valuable for cables manufactured from dissimilar metals where galvanic corrosion accelerates deterioration in moist environments. Field performance data from installations spanning multiple decades demonstrates the reliability and longevity achievable with quality waterproof cable sleeve products, providing confidence for critical infrastructure projects where connection failure carries significant consequences. Maintenance simplicity throughout the service life represents an often-overlooked advantage, as properly protected connections require minimal inspection and virtually no preventive maintenance beyond periodic visual verification. This maintenance reduction translates into substantial labor savings and operational efficiency improvements over extended timeframes, particularly for installations in difficult-access locations or harsh environments where maintenance activities prove costly and time-consuming.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000